What Is Belt Conveying Equipment and How Does It Work?
Belt Conveying Equipment moves bulk materials and packaged products along a continuous path. It uses a flexible belt, powered pulleys, support rollers, and a controlled drive system. Materials travel steadily between loading and discharge points. This simple movement supports mining, manufacturing, agriculture, warehousing, and many other industries.
The belt usually rests on rollers or a flat support surface. A motor turns the drive pulley, creating friction against the belt. That friction carries the load forward. Tensioning devices keep the belt aligned and reduce slipping during operation. At the loading zone, skirts and impact beds can limit spillage and protect the belt from sharp materials.
Small details matter.
A reliable conveyor requires suitable belt width, speed, capacity, and material compatibility. Operators should also inspect fasteners, rollers, guards, and emergency-stop devices regularly. In practical workplaces, dust, moisture, uneven loading, and temperature changes can affect performance. A system that works well on paper may need adjustment after installation. That is an important limitation often overlooked.
Experienced maintenance teams watch for belt mistracking, unusual noise, rising motor temperature, and material buildup. These signs can reveal problems before they cause costly downtime. Professional design should consider the full route, including transfer points, inclines, cleaning access, and worker safety. No conveyor is maintenance-free. Even durable equipment needs inspection, accurate installation, and sensible operating practices. Understanding these principles makes it easier to choose, operate, and improve Belt Conveying Equipment for dependable material handling.
What Is Belt Conveying Equipment?
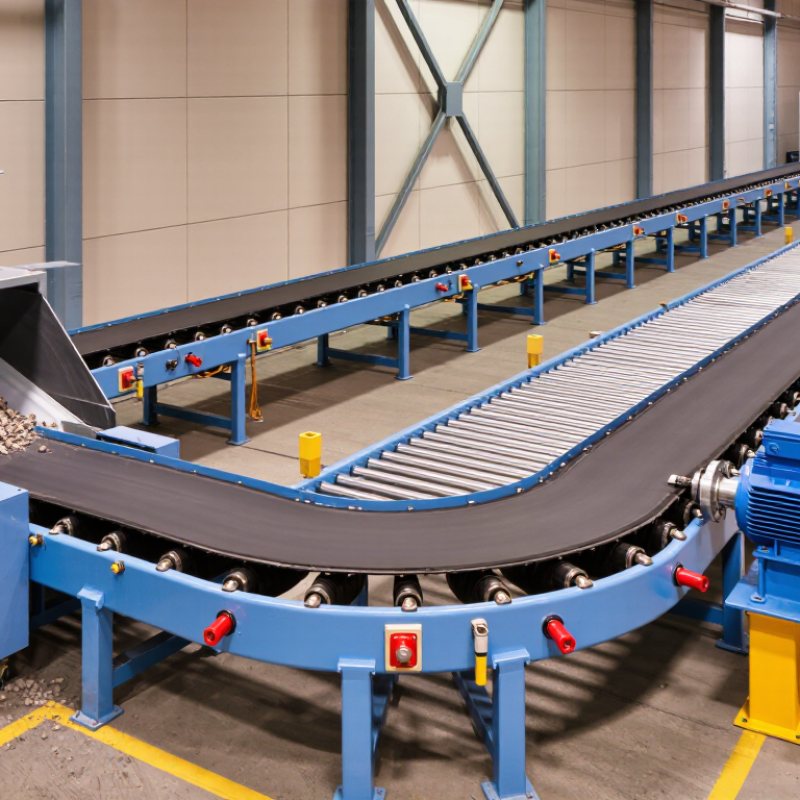
Belt conveying equipment is a mechanical system that moves materials along a continuous belt. It usually includes a belting surface, drive pulley, return pulley, support rollers, frame, and tensioning device. The belt may carry boxes, mineral fragments, grain, or packaged products. Its design changes with the material, distance, speed, and working environment.
An electric motor turns the drive pulley. Friction between the pulley and belt pulls the belt forward. Rollers support the loaded section and reduce sag. The return side travels underneath, often with fewer supports. At the discharge end, the material leaves the belt through controlled movement, not sudden lifting. Guards, emergency stops, belt cleaners, and alignment sensors improve operating safety and reliability.
The equipment looks simple.
In practice, small details matter. A belt running only slightly off-center can rub the frame and wear its edge. Excessive tension can damage bearings, while insufficient tension may cause slipping. Moisture, dust, sharp materials, and temperature changes also affect performance. Maintenance teams should check pulley surfaces, roller rotation, belt joints, and buildup regularly. One common mistake is selecting capacity from belt width alone. Load density and feeding conditions matter too. A careful design still needs review after installation, because real material flow rarely matches every original assumption.
What Is Belt Conveying Equipment and How Does It Work?
| Data Dimension | What It Is | How It Works | Typical Facts and Considerations |
|---|---|---|---|
| Basic Definition | A belt conveyor is a mechanical handling system that continuously transports materials on a moving belt. | An endless belt travels around rotating pulleys while carrying materials from one point to another. | It can move packaged goods, bulk solids, containers, components, and other materials over short or long distances. |
| Conveyor Belt | The flexible carrying surface that supports and moves the transported material. | The belt receives motion from the drive pulley and returns along the lower side of the conveyor frame. | Common belt materials include rubber, PVC, polyurethane, and fabric-reinforced elastomers. Material selection depends on temperature, abrasion, oil, food-contact, and chemical requirements. |
| Drive Pulley | The powered pulley that transfers rotational force to the belt. | An electric motor and gearbox rotate the pulley; friction between the pulley surface and belt produces belt movement. | Drive pulleys are commonly located at the discharge end, although the arrangement can vary by conveyor design. |
| Head Pulley | The pulley positioned near the material discharge point. | As the belt passes around the head pulley, the conveyed material leaves the belt and falls or transfers to the next process. | The head pulley may also serve as the drive pulley in many conveyor arrangements. |
| Tail Pulley | The pulley located at the loading or return end of the conveyor. | It guides the belt back toward the loading area and helps maintain the belt loop. | Some designs use an adjustable tail pulley to assist with belt tracking and tensioning. |
| Idler Rollers | Unpowered rollers that support the belt and its load. | They rotate as the belt passes over them, reducing sag and rolling resistance. | Carrying idlers support the loaded section; return idlers support the empty belt on its underside. |
| Carrying Idler Arrangement | The roller configuration beneath the loaded carrying side of the belt. | Flat idlers support a flat belt, while troughed idlers form a shallow channel that helps retain bulk material. | Typical trough angles include approximately 20, 35, or 45 degrees, depending on the design and material-handling requirements. |
| Conveyor Frame | The structural framework that supports pulleys, idlers, the belt, and protective components. | It maintains alignment and provides the required elevation, length, and support for the conveyor route. | Frames may be constructed from steel, stainless steel, or aluminum, depending on load, environment, hygiene, and corrosion requirements. |
| Motor and Gearbox | The power unit that supplies controlled rotational force to the drive pulley. | The motor produces rotation, while the gearbox generally reduces speed and increases usable torque at the drive pulley. | Required power depends on belt speed, conveyor length, incline, material mass, friction, acceleration, and operating duty. |
| Belt Tensioning System | A mechanism that maintains suitable tension in the belt. | Take-up devices compensate for belt stretch and help preserve contact between the belt and drive pulley. | Common approaches include screw take-ups, gravity take-ups, and automatic tensioning systems. |
| Belt Tracking | The process of keeping the belt centered along the conveyor structure. | Correct pulley alignment, idler positioning, belt tension, and tracking devices help prevent sideways belt movement. | Poor tracking can cause edge damage, material spillage, increased wear, and unplanned downtime. |
| Loading Zone | The area where material is placed onto the moving belt. | Chutes, hoppers, skirts, and impact idlers control the material flow and reduce the force of falling material. | Proper loading should be centered, steady, and aligned with the belt direction to minimize spillage and belt damage. |
| Discharge Zone | The area where material leaves the conveyor. | Material typically discharges at the head pulley or transfers to another conveyor, screen, bin, or processing machine. | Discharge behavior depends on belt speed, pulley diameter, material properties, and the transfer-point design. |
| Belt Speed | The linear speed at which the belt travels. | Speed is controlled by the drive system and determines how quickly material moves through the conveying route. | Many industrial conveyors operate at speeds ranging from below 0.5 m/s to several meters per second; the correct value depends on the material and application. |
| Load Capacity | The amount of material the conveyor can transport safely and continuously. | Capacity is influenced by belt width, belt speed, material density, cross-sectional loading, incline, and equipment design. | Capacity is commonly expressed in tonnes per hour for bulk materials or units per minute for packaged products. |
| Belt Width | The usable transverse width of the conveyor belt. | A wider belt can carry a larger cross-sectional load or provide more space for individual products. | Typical industrial belt widths vary from narrow belts used for small products to wide belts used for heavy bulk handling. |
| Incline and Decline Operation | The ability to transport material upward or downward between different elevations. | Inclined conveyors use belt friction, suitable loading, and sometimes cleats or raised profiles to reduce sliding. | The allowable angle depends on belt surface, material shape, moisture, particle size, and whether the material is packaged or loose. |
| Cleated Belt | A belt fitted with raised transverse profiles or cleats. | The cleats help retain products or bulk material when the conveyor operates on an incline or decline. | Cleat height and spacing should match the material characteristics and the required conveying angle. |
| Skirt Boards | Sealing plates installed along the sides of a loading area. | They contain material during transfer and reduce spillage before the load becomes evenly distributed on the belt. | Skirt contact should be adjusted carefully because excessive pressure can increase belt wear and drive resistance. |
| Safety Features | Devices and guards designed to reduce operational risks. | Emergency pull cords, guards, interlocks, alarms, and accessible stop controls allow the conveyor to be stopped or isolated during unsafe conditions. | Safety provisions should follow applicable workplace regulations, risk assessments, and site-specific procedures. |
| Energy Use | The electrical power required to operate the conveyor. | Energy is mainly used to overcome belt and idler resistance, lift material, accelerate the load, and overcome friction in the drive system. | Efficient loading, correct belt tension, aligned components, and properly maintained rollers can reduce energy consumption. |
| Routine Maintenance | Inspection and servicing activities used to keep the conveyor reliable. | Operators inspect belt condition, tracking, pulley lagging, idlers, fasteners, drive components, guards, and emergency-stop devices. | Maintenance intervals depend on operating hours, load, dust, moisture, temperature, material abrasiveness, and manufacturer specifications. |
| Primary Advantages | The operational benefits of belt conveying equipment. | Continuous belt movement provides a controlled path for transporting materials between processes. | Advantages commonly include continuous operation, relatively low noise, adaptable layouts, gentle product handling, and suitability for automation. |
| Common Limitations | Conditions that may restrict conveyor performance. | Material properties, excessive incline, poor loading, belt misalignment, or unsuitable environmental conditions can reduce performance. | Potential issues include belt wear, spillage, carryback, product degradation, limited flexibility around obstacles, and the need for regular maintenance. |
We have over 30 years of experience in designing complete hydraulic systems, repairs and distribution of fluid power equipment and parts.
FOLLOW US ON :
Contact Details
Address:
4020 SE 45th CT.
Ocala, FL 34480
Phone No:
Email:
sales@cunninghamfluidpower.com